
The Technology Stack Behind a High OAMI Score
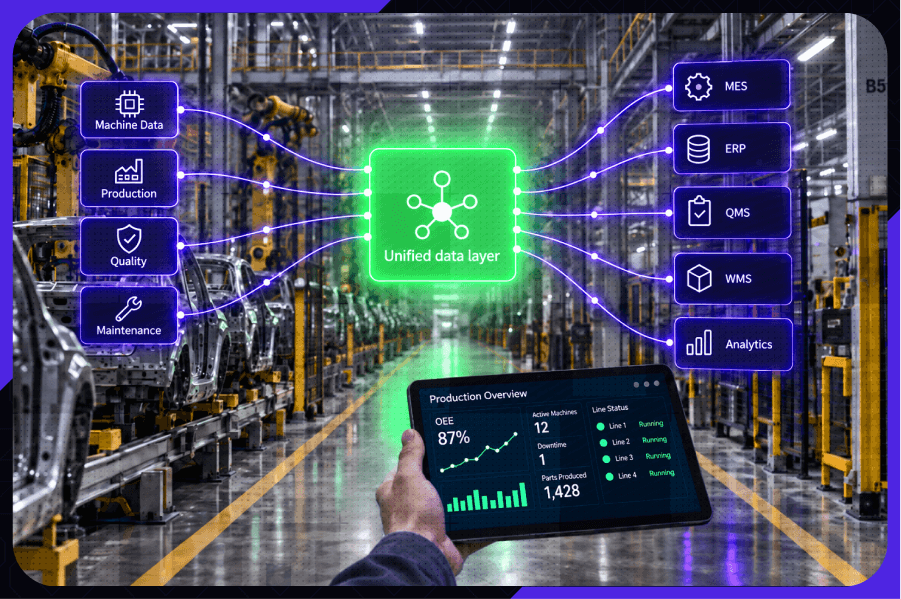
For automotive suppliers looking at an OAMI assessment, knowing the current score is only the beginning. The more difficult question is which manufacturing technologies and infrastructure can support the transition from isolated automation to a more connected operation.
OAMI focuses on the progression toward more automated, connected, and adaptive manufacturing environments. The specific technology stack can vary by facility, existing infrastructure, production needs, and current level of automation maturity.
However, several technologies commonly support that progression. Connected production equipment, Manufacturing Execution System (MES) and Supervisory Control and Data Acquisition (SCADA), integrated OT and IT data, predictive analytics, digital simulation, and automated quality processes provide the infrastructure manufacturers need to make production increasingly visible, coordinated, and responsive.
What OAMI Measures on the Plant Floor
OAMI measures the maturity of automation and digital connectivity across a supplier's manufacturing operation, progressing from predominantly manual production toward an integrated smart factory environment.
The five reported OAMI levels are Manual, Basic Mechanization, Semiautomation, Integrated Automation, and Smart Factory. GM has reportedly established a target of approximately 4.5 out of 5, although it has characterized its OAMI metrics as goals rather than formal requirements. GM has also not published a detailed public rubric defining the exact technology required at each level.
That distinction matters when evaluating the technology stack.
An automated machine does not necessarily create a highly mature manufacturing environment. A plant may have robots, CNC machines, automated inspection equipment, or other sophisticated assets, yet still rely on spreadsheets, manual data entry, disconnected applications, and human intervention to move information between systems.
Greater maturity comes from making those individual capabilities work together.
MES and SCADA: The Operational Core
MES and SCADA provide an operational foundation for many of the capabilities associated with more mature, connected manufacturing.
SCADA systems supervise and collect information from plant-floor equipment and controls. This can include machine states, cycle times, temperatures, pressures, alarms, and other process conditions. MES operates above the equipment layer, connecting production activities to information such as work orders, materials, quality events, production status, and scheduling.
Together, these systems help turn machine activity into usable manufacturing information.
Digital Twins and a Unified Data Foundation
Digital twins create virtual representations of physical equipment, production lines, or manufacturing processes, enabling manufacturers to simulate, test, and optimize operations before making changes to the physical production environment.
Digital twins rely on connected manufacturing data to reflect how equipment and processes behave under real operating conditions. Depending on the application, they can incorporate machine states, cycle times, process parameters, production rates, quality results, and other operational data to model different scenarios.
Manufacturers can use digital twins and simulation for applications such as assembly-station design, throughput modelling, process validation, robotics, bottleneck analysis, and quality prediction. For example, a manufacturer could simulate a proposed production change to identify its potential impact on cycle time or throughput before implementing it on the plant floor.
As manufacturing environments become more connected, digital twins can help turn operational data into a tool for testing and continuous improvement. They are not a confirmed OAMI requirement, but they represent the type of data-driven capability associated with more advanced Industry 4.0 manufacturing.
What Predictive Maintenance Requires
Predictive maintenance uses equipment condition data and historical performance information to identify potential failures before they cause unplanned downtime.
That requires more than installing sensors.
A predictive maintenance program needs reliable asset records, maintenance histories, condition-monitoring data, and enough historical information to identify meaningful patterns. Depending on the asset, manufacturers may collect vibration, temperature, electrical, pressure, acoustic, or other condition data.
That information can then flow through edge devices, historians, maintenance systems, MES, or analytics platforms to identify abnormal conditions and help maintenance teams intervene before equipment fails.
This creates a natural progression in maintenance maturity. Plants can move from reactive maintenance to scheduled preventive maintenance, then condition-based monitoring, predictive maintenance, and eventually more prescriptive approaches in which systems recommend actions based on predicted conditions.
Predictive Maintenance Metrics
GM has not publicly identified specific predictive maintenance metrics as OAMI scoring criteria. However, several manufacturing KPIs can indicate whether maintenance is becoming more proactive, connected, and data-driven.
Mean Time Between Failures (MTBF) measures the average operating time between equipment failures. Increasing MTBF can indicate improving asset reliability.
Mean Time to Repair (MTTR) measures the time required to restore equipment after a failure. Lower MTTR indicates that equipment is being returned to service more quickly.
Unplanned downtime measures production time lost to unexpected equipment failures. Predictive maintenance should help reduce avoidable downtime by identifying developing problems earlier.
The planned maintenance percentage compares planned maintenance work to reactive maintenance activity. A shift toward planned work can indicate that maintenance is becoming less dependent on emergency responses.
Overall Equipment Effectiveness (OEE) combines availability, performance, and quality to measure how effectively manufacturing equipment is being used.
The value of these metrics increases when they are calculated from machine-connected data rather than reconstructed manually after the fact. Automated data collection gives maintenance and operations teams a more timely view of equipment performance and creates the historical dataset needed for increasingly sophisticated analytics.
How Connected Manufacturing Data Improves Quality
Connected manufacturing data can turn quality information from a historical record into an active part of production control.
One example is part-level traceability. Digital traceability can associate a component or finished product with the materials, equipment, process conditions, inspection results, and production events involved in its manufacture. If a problem occurs, manufacturers can use that information to identify affected production more precisely.
A second capability is closed-loop quality. In a connected environment, an inspection result need not remain within a standalone quality system. The result can trigger an alert, workflow, containment action, or potentially a process adjustment.
The key difference is the speed at which high-quality information flows back into manufacturing.
OT Cybersecurity at Higher Maturity
Greater manufacturing connectivity also creates a larger cybersecurity surface area for manufacturers to manage.
Connecting PLCs, sensors, SCADA, MES, ERP, cloud applications, edge devices, and other systems creates additional pathways for operational data to flow. As OT and IT become more integrated, manufacturers need security controls designed for industrial environments rather than relying solely on conventional enterprise IT protections.
ISA/IEC 62443 provides a framework specifically for industrial automation and control system security, while NIST Cybersecurity Framework 2.0 addresses broader organizational cybersecurity risk, including supply chain risk management.
Cybersecurity has not been publicly identified as an OAMI scoring criterion. It is better understood as an architectural consideration that becomes increasingly important as plants add the connectivity required for advanced automation.
A connected factory cannot be treated as mature if the architecture enabling that connectivity cannot be operated securely and reliably.
How Industry 4.0 Is Shaping OAMI
Industry 4.0 has shifted manufacturing automation from individual automated machines to connected systems that integrate equipment, software, data, analytics, and, increasingly, AI.
In a traditional automation environment, machines may perform tasks automatically but still operate within separate systems. Industry 4.0 environments connect machines to production, quality, maintenance, inventory, and enterprise data, enabling information to flow across the operation in real time.
This changes how automation maturity is evaluated. Higher maturity increasingly depends on capabilities such as real-time production visibility, connected equipment, integrated OT and IT systems, automated data collection, predictive analytics, digital traceability, and faster feedback between production and quality systems.
OAMI reflects this broader shift by evaluating how far supplier operations have progressed from manual or partially automated production toward increasingly connected and adaptive manufacturing environments.
For suppliers, that means automation maturity depends not only on adding more equipment or robotics, but also on how effectively manufacturing systems share data and coordinate decisions across the plant.
How Ford's Framework Compares to OAMI
Ford's supplier framework approaches manufacturing maturity differently from GM's OAMI initiative, but many of the same underlying technologies can support both.
Ford uses programs, including Q1 certification and Materials Management Operations Guideline/Logistics Evaluation (MMOG/LE), to evaluate supplier capabilities. MMOG/LE, developed by the Automotive Industry Action Group (AIAG) and Odette, focuses on materials management and supply chain processes, including capacity planning, production control, customer and supplier interfaces, and operational coordination.
OAMI has a more direct focus on automation and connectivity within supplier operations. That makes technologies such as MES, connected production data, digital traceability, integrated quality systems, and real-time production visibility more central to the discussion of maturity.
Even though Ford's framework does not score automation in the same way, those technologies can still support the processes its supplier programs evaluate. For example, integrated manufacturing systems can improve production visibility, strengthen traceability, support capacity planning, and provide more reliable operational data across quality, materials, and logistics workflows.
For suppliers serving both OEMs, this creates significant technology overlap. A connected manufacturing architecture can support OAMI-style automation maturity while also strengthening the process control, data visibility, and supply chain execution expected across other automotive supplier frameworks.
Connect Your Technology Stack With Fuuz
Building greater automation maturity depends on connecting equipment, systems, and manufacturing data so they can work together across the operation.
Fuuz provides an ERP-agnostic manufacturing platform that brings MES, WMS, QMS, maintenance, connected worker functionality, and no-code/low-code automation into a unified environment. Prebuilt ERP connectors can help manufacturers integrate existing enterprise and plant-floor systems without requiring every current technology investment to be replaced.
For automotive suppliers evaluating OAMI readiness, Fuuz can help create the connected operational foundation needed to improve visibility, standardize processes, and support increasingly integrated manufacturing.
Contact Fuuz to discuss the technology architecture behind greater automation maturity.